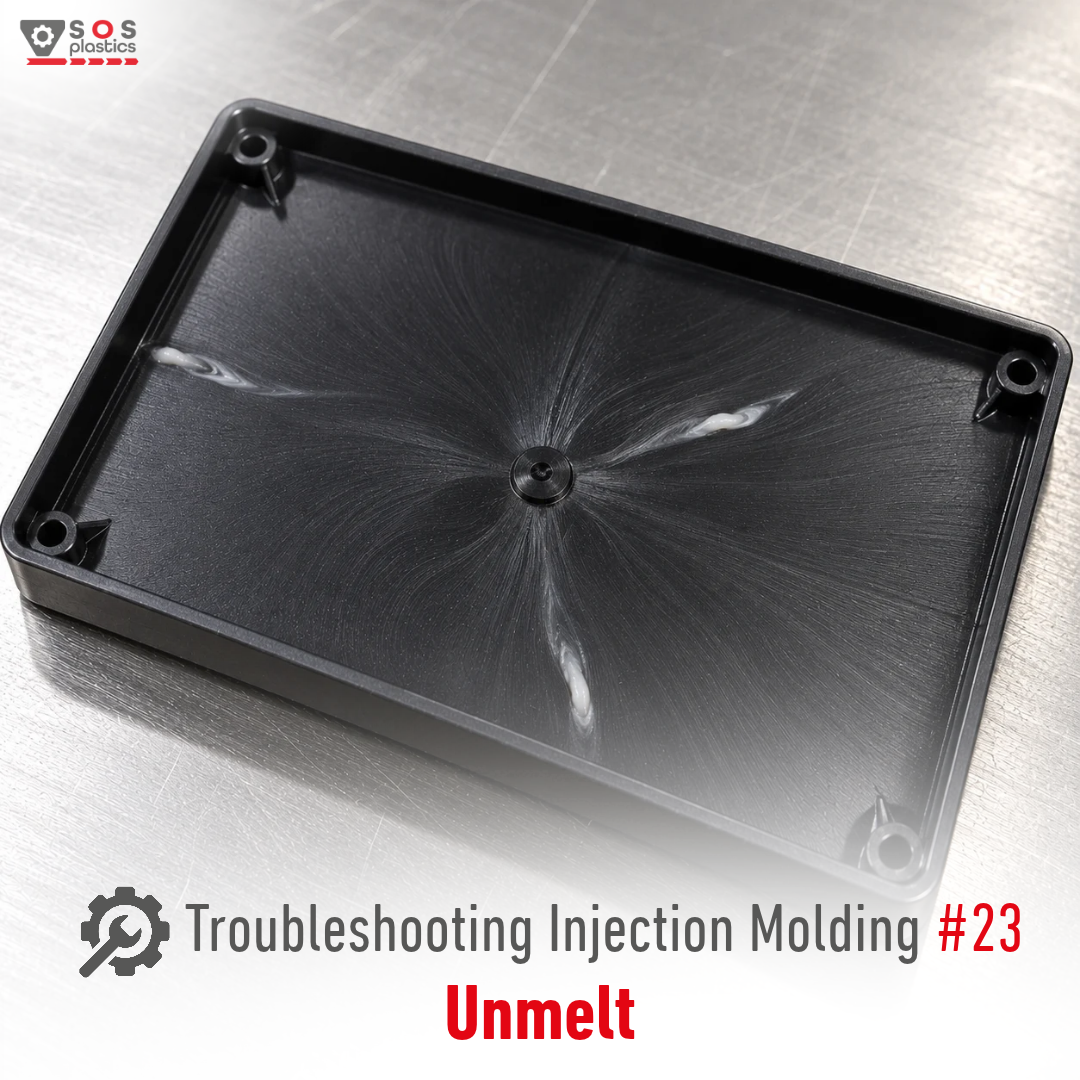
Unmelt (also referred to as unmelted particles or, in some references, pitting) occurs when incompletely melted polymer particles remain visible in the molded part. The defect may appear as small, localized surface imperfections and can be particularly noticeable in pigmented components.
When troubleshooting Unmelt, investigate the causes in the right order:
1️⃣ The melt temperature is too low
➡️ Verify the actual melt temperature, not just the machines setpoints.
➡️ Increase the melt temperature within the material suppliers recommended processing window if required.
2️⃣ The barrel temperature profile is incorrect
➡️ Check the temperature profile across all barrel zones.
➡️ Adjust the profile according to the materials melting behavior and processing recommendations.
3️⃣ The injection unit is too large for the shot size
➡️ Check the shot volume in relation to the injection units capacity.
➡️ Where appropriate, increase the shot utilization or consider a more suitable injection unit. Verify the actual residence time before making changes.
4️⃣ Back pressure is too low or screw speed is too high
➡️ Check back pressure and screw rotation speed.
➡️ Increase back pressure or reduce screw speed as appropriate to improve melt quality. Change one parameter at a time and monitor the actual melt temperature.
5️⃣ The regrind contains oversized particles
➡️ Inspect the regrind for inconsistent particle size, oversized granules and poor grinding quality.
➡️ Improve grinding consistency, reduce the proportion of regrind where necessary, and verify whether the defect disappears when using suitable virgin material.
6️⃣ The material is contaminated with another polymer
➡️ Check the material supply, hopper, conveying system, dosing equipment and regrind handling process for cross-contamination.
➡️ Purge and clean the affected equipment where necessary. Verify material identity and segregation before restarting production.
⚠️ Increasing the melt temperature is not always the answer. Excessive temperatures or residence times can degrade the polymer and create new defects.
⚠️ If the defect persists despite correct processing conditions, investigate screw design, wear and the machines ability to melt and homogenize the material consistently.
Next in the Plastic Troubleshooting Series:
➡️ Brittleness
Have you ever solved an Unmelt problem by changing the barrel temperature profile rather than simply increasing the melt temperature?